Shell thickness isn't just a number on a drawing — it's the result of a chain of engineering decisions. This article walks the same path the technical office walks for every project.
The datasheet: where it actually starts
Every pressure vessel starts with a datasheet, not a thickness number. At minimum it needs design pressure, working temperature, fluid type and density, required volume, corrosion allowance, and installation conditions. Until those are set, no thickness number is defensible.
Design pressure is usually set above working pressure — typically 10% higher or at least one extra bar — to cover network fluctuations and relief-valve behaviour.
Allowable stress and material choice
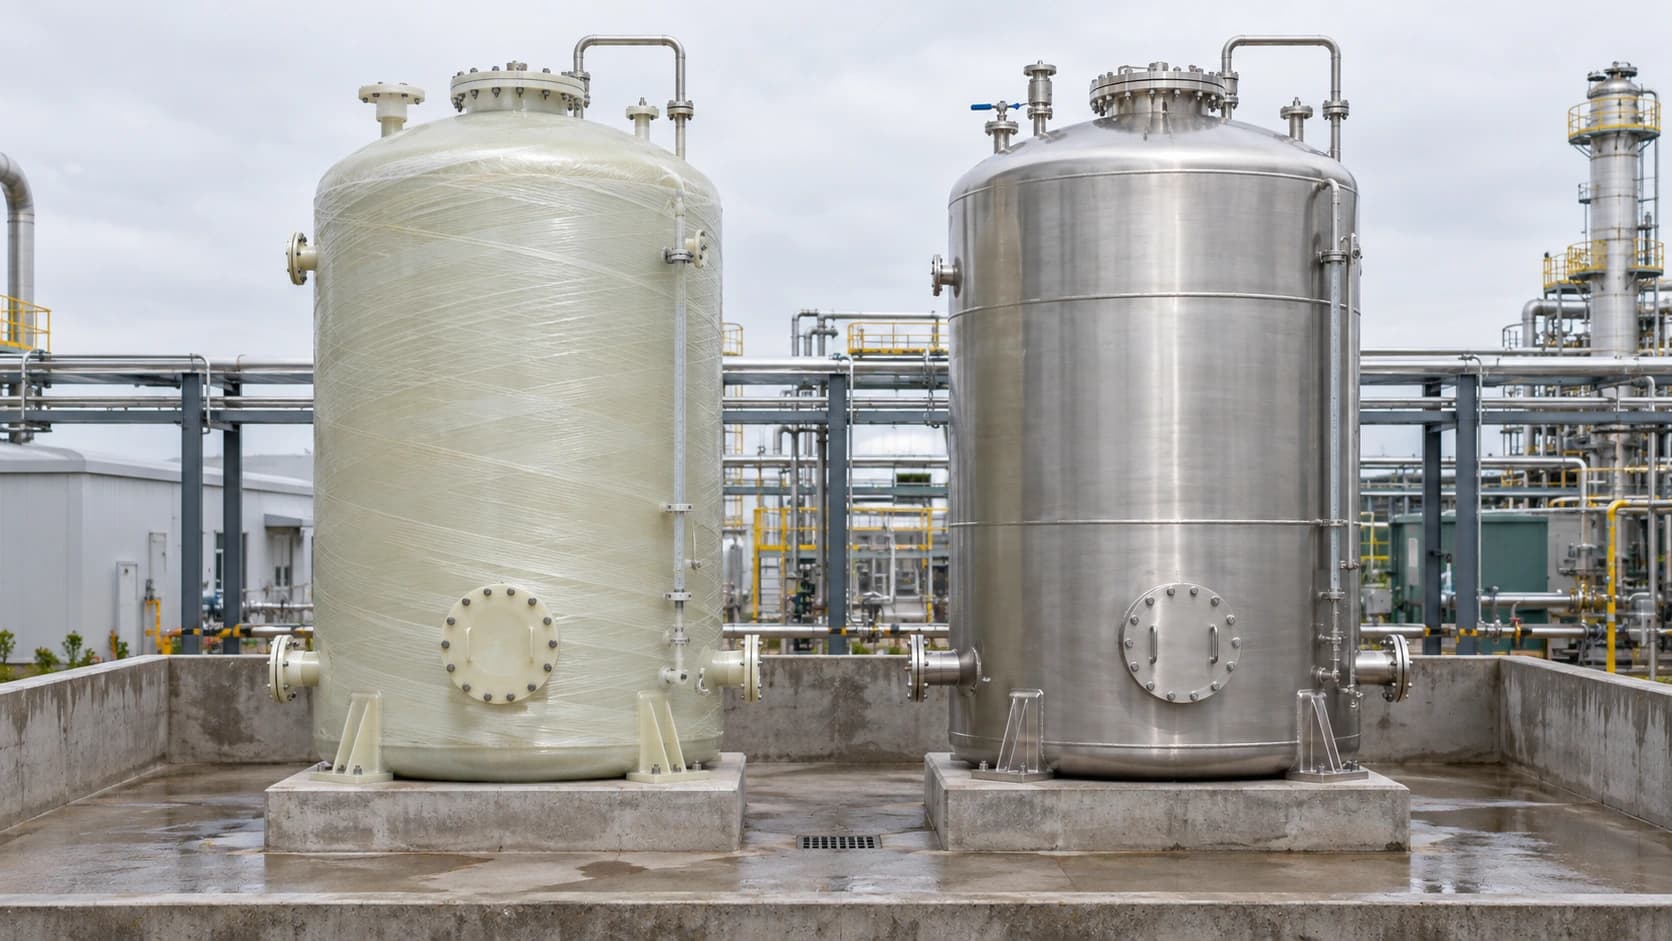
The material's allowable stress at design temperature comes straight from the code's tables and feeds directly into thickness. Carbon steel usually suits compressed air and industrial water; corrosive or hygienic fluids call for stainless.
| Material | Common use | Suited temperature |
|---|---|---|
| A516 Gr.70 | Compressed air, industrial water | Up to ~200°C |
| ST37 | Low-pressure vessels | Up to ~120°C |
| SS 304 / 316 | Corrosive or hygienic fluids | Up to ~300°C |
The calculation order
- Set design pressure and temperature from the datasheet
- Pull the material's allowable stress at that temperature
- Pick a joint efficiency based on the radiography percentage
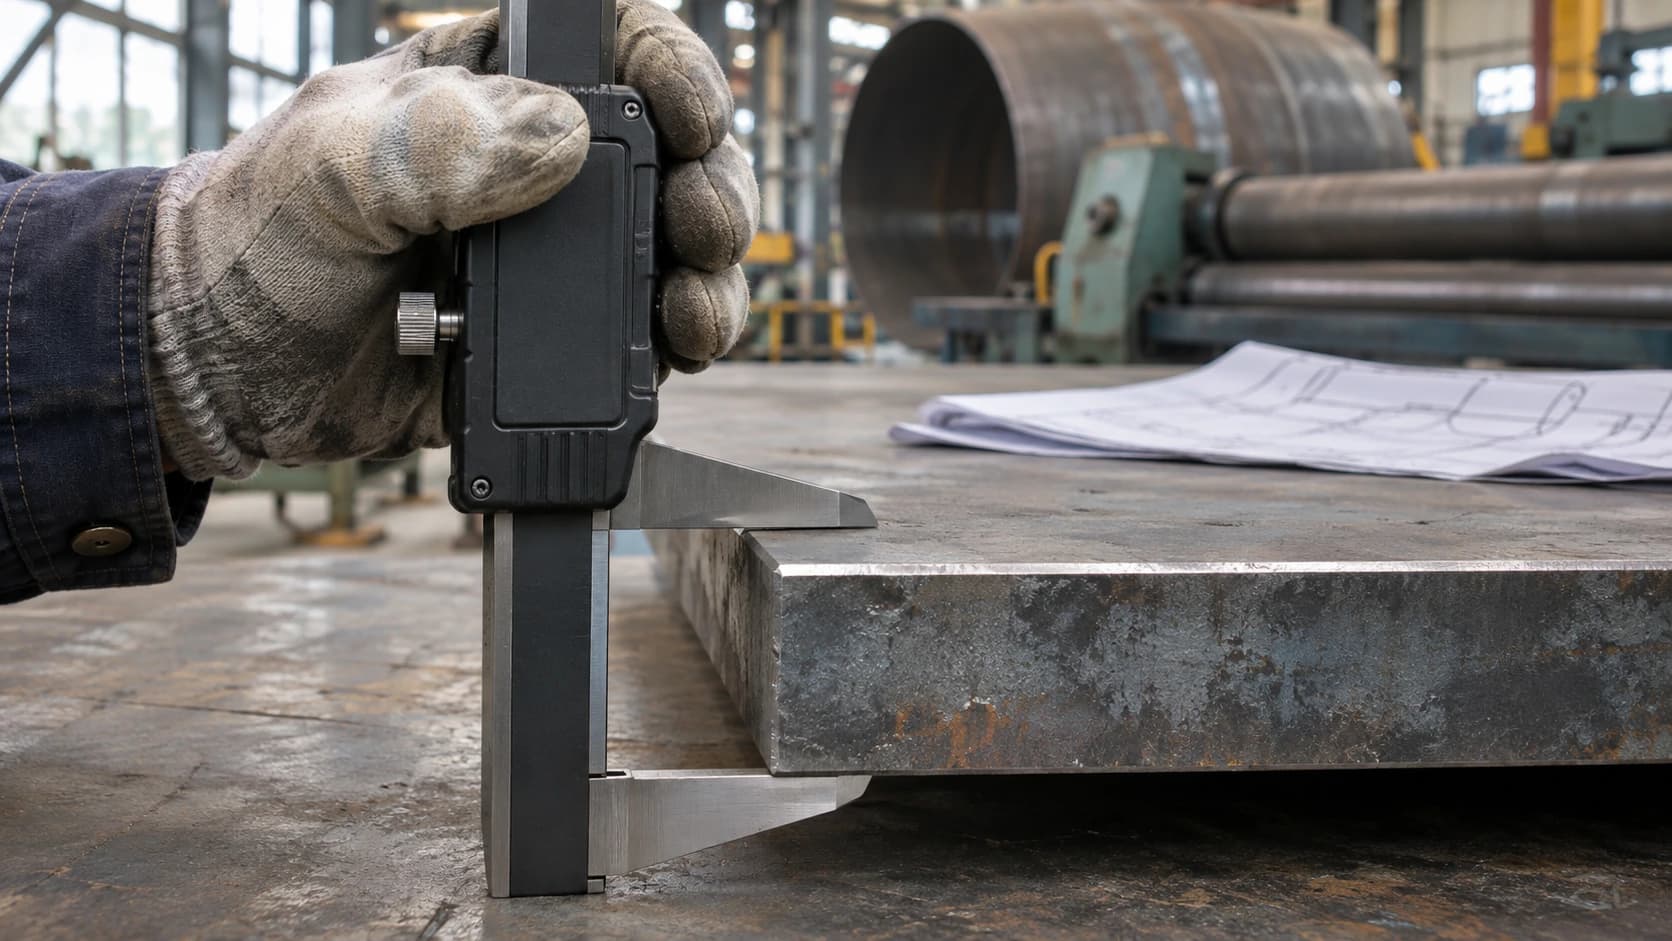
- Add corrosion allowance and round up to a stock plate thickness
Common mistakes
The most common one is skipping corrosion allowance: the vessel is sound on delivery day, but a few years into service its thickness drops below the calculated minimum. The second is picking a high joint efficiency without a matching radiography plan — third-party inspection rejects it.
From calculation to fabrication drawing
The final output is a calculation report paired with a fabrication drawing: shell and head thickness, nozzle layout, manway details, weld specification, and the inspection plan. That package goes to the shop floor and ends up as the vessel's technical file for the client.
Correct thickness is the result of a complete datasheet, the right material, a realistic joint efficiency, and a sensible corrosion allowance. Whichever of these four gets guessed will show up later — in inspection, or in the years of service that follow.